+86 15633683072
Most fabrication shops don't get this wrong because they chose a bad machine. They get it wrong because they chose the wrong type of machine for the joint, the position, and the production volume they actually run.
Two systems dominate the mechanized welding market: the welding track carriage that follows a mounted rail, and the magnetic welding carriage that runs directly on the workpiece. Both automate torch travel. Both improve consistency over manual welding. But they solve different problems on the floor, and picking the wrong one means fighting your equipment every shift.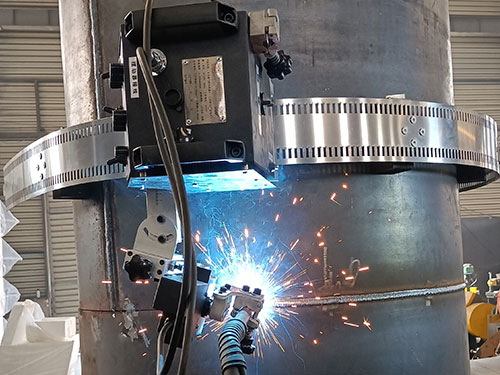
A welding track carriage rides on a guide rail—rigid, semi-flexible, or ring-shaped—mounted directly on or adjacent to the joint. The carriage follows a fixed path, which makes travel highly accurate and repeatable across long distances. Rigid rails handle long straight seams. Semi-flex rails cover gentle curves with a minimum radius around 5 meters. Ring rails are designed for circumferential welding on pipe and tube from 8 inches up to roughly 3 meters in diameter.
The Steelmax Rail Runner II is a useful reference point here: magnetic guide rail, rack-and-pinion drive, all-position capability, and an integrated linear oscillator with widths up to 50 mm and speeds up to 3000 mm/min. That level of spec control is why track systems dominate on pipe girth welding, pressure vessel shells, and structural steel runs where the same joint repeats hundreds of times.
The trade-off is setup. Installing and aligning the rail takes time. On a large pipe girth welding joint, that can easily consume 20 to 30 minutes before the first arc starts. For a one-off weld, that's hard to justify.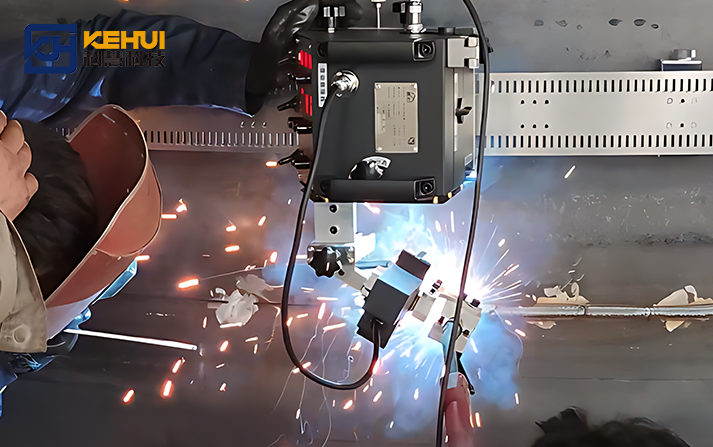
A magnetic welding carriage skips the rail entirely. It attaches to the workpiece with permanent magnets and travels using friction drive wheels or a magnetic track. The Gullco Magnetic MOGGY is a textbook example: a lightweight, four-wheel friction drive carriage with a magnetic base that clings to vertical members for out-of-position fillet welding, with infinite speed selection from roughly 8 to 255 cm/min.
Setup takes minutes, not tens of minutes. No rail installation, no alignment, no track removal. For field work, confined spaces, and mixed-production shops where the next joint might be a different size or orientation, that speed advantage is real. The standard MOGGY can also be reversed to run on a 6-inch V-groove track if you later need rail-guided travel—one machine covering both approaches.
The limitation is path geometry. Trackless systems excel on straight or gently curved seams. They follow the joint, but they don't provide the same rigid guidance as a mounted rail. On long, critical welds where the torch must hold exact position over several meters, the track carriage still wins.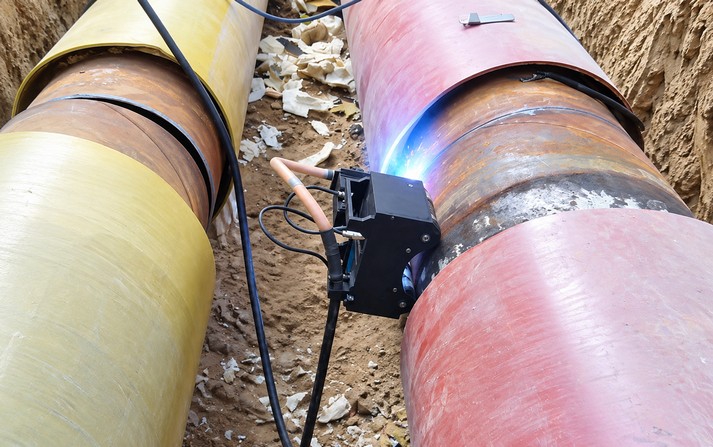
Ask three questions before choosing:
Is the seam long and straight? If yes, a welding track carriage with rigid rail gives you the most consistent torch position and the least operator intervention. This is the standard setup for welding carriage for structural steel welding—box columns, bridge girders, long stiffener runs.
Is the seam curved or circular? Ring rails on a track carriage handle pipe girth welding and tank circumferential seams with high repeatability. Flexible track welding carriage setups adapt to curved plates and tank shells. A magnetic welding carriage can handle large pipe girth welding on consistent OD, but if the pipe has significant ovality or the weld sits near a fitting, the magnetic grip becomes less predictable.
Is the joint in an awkward position? Vertical up, overhead, or confined spaces favor the magnetic welding carriage. The Gullco Magnetic MOGGY was specifically designed to run on a vertical path against a horizontal surface or a horizontal path against a vertical surface—out-of-position fillet welds that are brutal to do manually.
This is where the math gets uncomfortable for shops that buy the wrong system.
High-volume, repetitive work—the same joint, the same position, hundreds of times—is track carriage territory. The setup time amortizes across the production run. The rack-and-pinion drive and fixed rail mean every weld starts from the same reference point. On a pipe spooling line running consistent diameters, a flexible track welding carriage with a ring rail turns girth welding into a repeatable, almost boring process. That's the goal.
Low-volume, high-mix, or field work flips the equation. If your shop runs 5 to 20 joints per day across different sizes and orientations, rail setup becomes dead time. A magnetic welding carriage for large pipe girth welding on consistent OD lets you start welding in minutes and move to the next joint without rail teardown. The same applies to pressure vessel welding where you're moving between shell courses, nozzles, and stiffeners—the magnetic carriage follows you.
Magnetic adhesion depends on the workpiece being ferromagnetic. Carbon steel and most low-alloy steels work fine. Stainless steel, aluminum, and duplex materials do not—magnetic welding carriage systems are effectively off the table for those materials unless you're using a magnetic track as a rail (where the track provides the magnetic attachment to the structure, not the carriage itself).
Track systems don't care about material magnetism. A flexible track welding carriage mounts mechanically or magnetically and works on stainless, aluminum, and exotic alloys. That's a hard constraint, not a preference.
The UK Navy aircraft carrier project at Cammell Laird shipyard in Merseyside is a useful case study. The shipyard selected Gullco equipment after evaluating multiple vendors against military welding inspection standards. They used the KAT all-position track carriage for the majority of welding procedures—long continuous welds in flat position with oscillator head combinations—and Moggy trackless friction drive carriages for flat position fillet welds.
The mixed approach is telling. They didn't pick one system and force it onto every joint. Track carriage handled the long, critical structural runs. Trackless handled the fillet welds where setup speed mattered more than rail precision.
A fabrication shop manager running pressure vessel welding once described the real cost of rail setup this way: “The rail is 10 minutes. The alignment is 15. The teardown is 5. That's half an hour per joint that nobody invoices.” Multiply that by 200 joints and you've lost 100 hours of arc-on time.
But flip the scenario: the same manager running a 40-foot longitudinal seam on a storage tank shell. The rail goes up once. The carriage runs the full length in one continuous pass at controlled speed. The weld is perfect because the torch never wavered. The 30-minute setup is nothing against the 4-hour weld.
Same equipment category. Opposite economics. The welding carriage for pressure vessel welding that makes sense on a short nozzle ring is not the same system that makes sense on a full shell course.
| Your Situation | Better Choice | Why |
|---|---|---|
| Long straight seams (>2 m), repeated | Welding track carriage | Rail eliminates torch drift |
| Pipe girth welding, consistent OD | Flexible track welding carriage or ring rail | Repeatable circumference travel |
| Field work, varying joint locations | Magnetic welding carriage | Minutes to first arc |
| Vertical/overhead fillet welds | Magnetic welding carriage | Designed for out-of-position |
| Stainless or aluminum | Track carriage only | Magnetism doesn't apply |
| High-mix, low-volume shop | Magnetic welding carriage | Changeover is the bottleneck |
| High-volume pipe spooling | Track carriage with ring rail | Setup amortizes fast |
The honest answer for many shops is: you need both. A track carriage for the long, critical runs and a magnetic welding carriage for the fillets, the field work, and the changeover-heavy days. That's not a sales pitch—it's what the shipyard did on the carrier project, and what most serious fabrication shops eventually figure out.
On consistent pipe OD with good surface conditions, yes—especially for large pipe girth welding where rail installation around the circumference is time-consuming. But on pipes with significant ovality, fitting-heavy joints, or near flanges, the rail-guided welding track carriage still provides more consistent torch positioning.
A magnetic welding carriage typically mounts in 2–5 minutes. A welding track carriage with rigid rail and alignment runs 15–30 minutes depending on joint length and access. On a 10-joint day, that difference compounds fast.
Long structural seams—girders, columns, stiffeners—favor the track carriage. The rigid rail keeps the torch path straight over multiple meters. For shorter structural fillets in varied positions, the magnetic welding carriage is faster to deploy and equally capable.
Flexible track covers curved surfaces and tank shells where rigid rail can't conform. If your work is mostly flat plate or straight pipe, rigid rail is cheaper and equally precise. If you run tank circumferential seams or curved plate, the flexible track welding carriage earns its price.
Some systems support both. The Gullco MOGGY, for example, can reverse its wheel assemblies to run on standard V-groove track, giving you trackless operation and rail-guided travel in one carriage. It's not the same as a dedicated rigid-rail system for long seams, but it's a practical compromise for shops that need flexibility more than maximum precision.
Zhengzhou Kehui Technology Co., Ltd
Email: info@zzkehui.com


 Chinese
 English
 OA
 Current location:
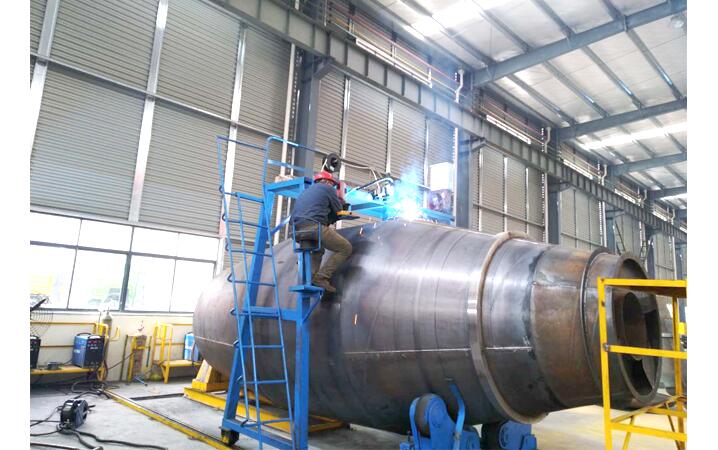 Concrete Mixer Drum Robotic Welding Solutions
 Automobile Body Production Line Welding Fixtures
 Automotive Body Welding Automated Manufacturing Solutions
 Free-Teaching Programming Welding Robot Cell For I Beam Welding
 No Programming Required Robotic Welding Systems for H beam Welding Line